RPE-G-N: A Specialized Polyethylene Powder Coating for the Inner Lining of Galvanized Pipes
Product description
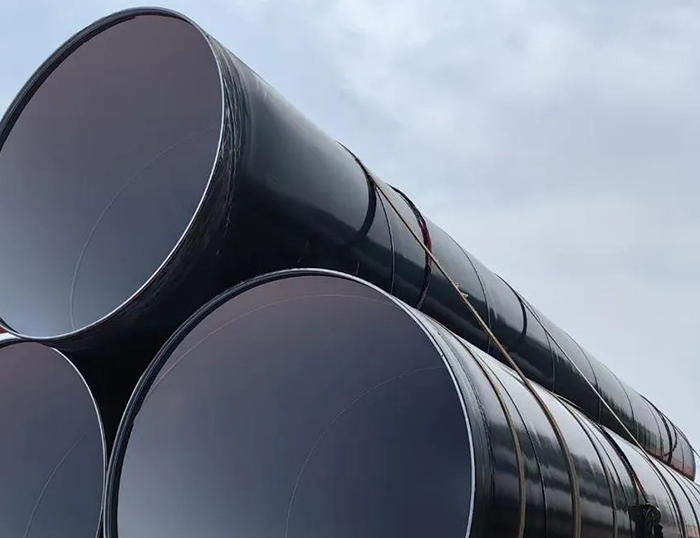
The specialized polyethylene powder coating for galvanized pipelines is a thermoplastic powder coating formulated with polyethylene resin, compatibilizers, functional additives, pigments and fillers. Having passed national quality inspections and health safety evaluations, it is fully suitable for coating water distribution equipment and pipelines used in ambient-temperature drinking water systems. This coating exhibits excellent chemical stability, electrical insulation properties, low-temperature resistance, as well as superior and long-lasting corrosion protection performance.
The product complies with the urban construction industry standard CJ/T120-2016 of the People's Republic of China.
Application area
Suitable for coating of water distribution equipment and pipelines for ambient temperature drinking water.
Application Instructions
Pre-treatment: Before plastic coating application, the base pipe must undergo sandblasting or acid washing and phosphating processes to remove rust, oil contaminants from the metal substrate surface, and oxide films from the galvanized layer surface.
Workpiece preheating temperature: 230–280°C [adjust according to pipe diameter];
Coating method: Vacuum dip coating
Plasticizing: 180–220°C, 0–5 minutes [The plasticizing process is determined based on pipe diameter specifications and coating smoothness; post-heating during plasticization facilitates the formation of a smooth coating on metal workpieces].
Cooling: Air-cooled or naturally cooled;
Film properties
|
Color |
GB/T 9761 |
No obvious visual difference was observed (when compared with the sample mold). |
|
Appearance |
Visual inspection |
Flat and smooth (slight orange peel texture allowed) |
|
Coating thickness μm |
GB/T 13452.2 |
250~600 |
|
Glossiness % |
GB/T 9754,60° |
10–80 (adjust according to customer’s specific requirements) |
|
Flexibility (membrane thickness 200 μm) |
GB/T 6742 |
≤2mm |
|
Low-temperature embrittlement |
Q/HJ 008-2008 |
No cracks observed at-35°C for 60 hours. |
|
Shore hardness (D) |
GB/T2411 |
45–55 (adjust according to customer’s specific requirements) |
|
Vicat softening point (°C) |
GB/T1633 |
85-95 |
|
Adhesion |
10 mm wide, 180° peeling |
≥30N/10mm (both coating tear and fragmentation tests confirm satisfactory adhesion) |
|
Tensile strength (MPa) |
GB/T 1040 |
>9.80 |
|
Elongation at break % |
GB/T1040 |
>300 |
|
Flattening test |
CJ/T120 |
No peel-off or fracture. |
|
Pipe fitting bending |
CJ/T120 |
No peel-off or fracture. |
|
Blow-test |
CJ/T 120 |
No peel-off or fracture. |
|
Sanitation Performance Testing |
GB/T 17219 |
Complies with the requirements of the Ministry of Health's "Hygienic and Safety Evaluation Specifications for Drinking Water Distribution Equipment and Protective Materials". |
|
Non-volatile content |
GB/T 2914 |
>99.5% |
Health and Safety
This powder coating is a non-toxic product; however, inhalation of dust should be avoided during application. Operators are advised to wear appropriate dust masks and protective goggles. If possible, prolonged skin contact with the powder coating should be minimized.
Note:
◆Excessive heating causes coating aging and discoloration, while the galvanized layer is also damaged by high temperatures; it compromises the adhesion between the coating film and the substrate. Conversely, insufficient heating leads to defects such as poor powder adhesion and uneven coating surface. Therefore, the optimal heating temperature should be determined through testing based on metal thickness and the customer's coating equipment specifications.
◆Adhesion is crucial to the quality of plastic-coated pipes, with workpiece pretreatment and application temperature being the primary factors influencing it; therefore, the coating process must be strictly controlled.
◆Workpiece Design: For straight seam welded steel pipes, internal burrs must be removed; the residual height of internal weld bead shall not exceed 0.5 mm.
◆This product is not recommended for use in post-processing applications (where the coated workpieces are subsequently reshaped). Like all polymer powders, this powder may ignite or burn, especially under flow conditions when exposed to high-temperature sources or ignition devices.